In the printed circuit board (PCB) manufacturing industry, solder mask window design—a critical factor affecting product quality and production efficiency—often serves as a major point of contention in communications between manufacturers and customers. In particular, customers’ specific requirements for the solder mask treatment of VIA holes (via holes)—such as full solder mask coverage, partial openings, or single-sided openings—can, if not handled properly, not only lead to production rework and increased costs but also cause serious issues such as soldering failures and signal interference down the line.
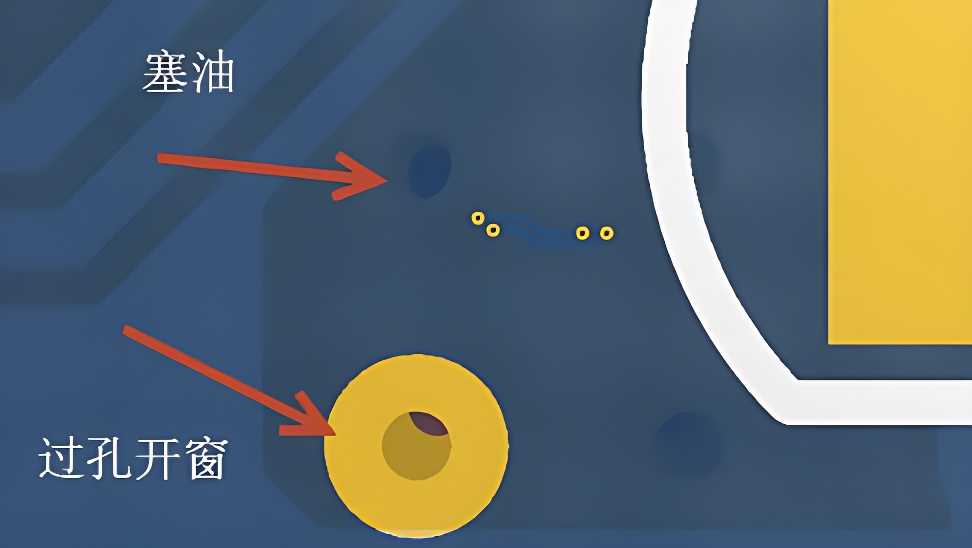
According to industry statistics, the PCB defect rate caused by improper green-oil window design accounts for 18%-25% of the total defect rate, directly affecting order delivery times and customer satisfaction.
As a professional PCB manufacturer, how can we effectively address the challenges of green solder mask window design and strike a balance between customer requirements and production feasibility? This article will provide industry professionals with practical technical guidelines and solutions—covering aspects such as the selection of surface treatment methods, key points for reviewing green solder mask window designs, process optimization strategies, and handling special scenarios—to help improve production efficiency and product yield.
I. Key Challenges in PCB Solder Mask Window Design: Analyzing the Conflict Between Customer Requirements and Production Constraints
In the PCB manufacturing process, the primary function of solder mask is to protect copper foil circuits, prevent oxidation and corrosion, and avoid soldering short circuits. Solder mask openings, on the other hand, are exposed areas reserved for critical regions such as pads, test points, and VIA holes, and they directly impact subsequent assembly and electrical performance. Currently, the challenges customers face with solder mask window design are primarily concentrated on the handling of VIA holes, which can be categorized into three types:
(1) VIA holes fully covered with green solder mask (no openings)
Some customers, due to product sealing and dust-proofing requirements, request that VIA holes be completely covered with solder mask, without leaving any openings. Although this design enhances the protection of the PCB surface, it can lead to two major issues during production: First, after the green solder mask cures, it may block the vias, preventing solder from penetrating during subsequent through-hole soldering and affecting electrical conductivity; Second, if a tin-plating surface treatment is used, the high-temperature molten tin may react with the solder mask inside the holes, causing bubbles or peeling and damaging the protective solder mask layer.
(2) Localized VIA Hole Opening (Partial Exposure)
To balance protection and soldering requirements, customers often request that VIA holes be opened only in specific areas (such as exposing the outer third of the hole’s edge). The challenge with this design lies in controlling the precision of the windowing—if the windowed area is too small, the effective pad area will be insufficient, leading to cold solder joints during soldering; if the windowed area is too large and exceeds design standards, too much copper foil will be exposed, increasing the risk of oxidation and short circuits. In addition, localized exposure may cause uneven adhesion between the solder mask and the substrate, leading to cracking during subsequent high- and low-temperature testing.
(3) VIA with single-sided window (exposed only on the front or back side)
Single-sided window designs are commonly found in PCB products with single-sided soldering or special structures (such as the need for localized electrical connectivity in multilayer boards), but this design places extremely high demands on process compatibility. If the surface treatment method is chosen improperly (such as tin plating), the VIA holes in single-sided windows are prone to forming “tin balls” during production— — that is, molten tin seeps into the hole on the side without a window and forms metal particles upon cooling. This not only affects the appearance but may also cause the particles to detach during use, leading to circuit short circuits.
To address these challenges, manufacturers need to adopt an approach that involves “first determining the surface treatment and then optimizing the green ink process,” thereby mitigating production risks at the source while meeting customers’ personalized needs.
II. Surface Treatment Methods: The “Pre-Filter” Designed by Green Oil Window”
PCB surface treatment is a key factor in determining the feasibility of the green solder mask window process. Differences in temperature and chemical properties among various treatment methods directly affect the compatibility of green solder mask treatment for VIA holes. Manufacturers must first identify the type of surface treatment selected by the customer before developing a corresponding green solder mask window solution. The specific classifications and compatibility are as follows:
(1) Hot Air Solder Leveling (HASL): The “No-Go Zone” for Single-Sided Plugged-Hole Processes”
Solder spraying is a widely used surface treatment method in the industry. It works by applying a molten tin-lead alloy (or lead-free tin alloy) evenly to the surface of a PCB at high temperatures (approximately 240–260°C) to form a protective layer. However, the high temperatures involved in the tin-spraying process create an inherent conflict with single-sided VIA plugging (single-sided solder mask coverage):
- The Risk of Thesis Plagiarism: The filling depth of green solder paste in single-sided plated-through holes is typically only 1/2 to 2/3 of the hole depth, and the areas not filled with green solder paste form “voids.” During the tin plating process, molten tin at high temperatures easily penetrates these voids and solidifies upon cooling into tin beads with diameters of 0.1–0.3 mm. If these tin beads remain inside the holes or on the surface, they will be deemed cosmetic defects by customers and must be manually removed, increasing production time.
- The Risk of Green Paint Peeling Off: The high temperatures involved in tin plating can weaken the bond between the green solder mask on single-sided filled vias and the substrate. This is particularly true at the edges of the vias, where the green solder mask is prone to peeling or flaking, exposing the copper foil and increasing the risk of oxidation. According to test data, under the tin-spraying process, the solder mask delamination rate for single-sided filled vias reaches as high as 12%, which is significantly higher than the 3% rate for double-sided filled vias.
Conclusion: If a customer chooses tin plating as the surface treatment, designs featuring single-sided VIA plugging (single-sided windowing + solder mask coverage) must be strictly prohibited. It is recommended to switch to double-sided plugging or a fully open-window process to fundamentally prevent issues with solder balls and solder mask delamination.
(2) Electroless Nickel-Gold (ENIG): The “Ideal Partner” for Single-Sided Plugged Holes”
The electroless plating process uses chemical deposition to form a nickel layer (5–10 μm thick) and a gold layer (0.05–0.1 μm thick) on the surface of a PCB. It offers the advantages of high-temperature resistance, oxidation resistance, and low contact resistance, and the process temperature is only 80–90°C. and it is highly compatible with green solder mask:
- No risk of solder balls: The electroplating process does not require high-temperature metal melting, so molten tin does not seep into the vias. Even when vias are designed with single-sided plugging, this ensures that the vias remain clean and free of metal particle residue.
- High stability of green oil: The low-temperature process does not compromise the bond strength between the green solder mask and the substrate. The green solder mask with single-sided via filling maintains good adhesion even after electroless gold plating. Following high-low temperature cycling tests (–40°C to 125°C, 100 cycles), the cracking rate of the green solder mask is less than 2%.
Suitable Scenarios: The electroless gold plating process is suitable for high-precision, high-reliability PCB products (such as medical devices and communication modules). If a customer requires single-sided via exposure with solder mask coverage and has high requirements for soldering stability, electroless gold plating is the preferred surface treatment method.
(3) OSP (Organic Protective Layer): The “Best Value Choice” for Low-Cost Applications”
The OSP process provides short-term oxidation protection by forming a thin organic film (0.2–0.5 μm thick) on the surface of copper foil. It offers the advantages of a simple process, low cost, and lead-free, environmentally friendly characteristics. The process temperature is approximately 100–120°C, and it is highly compatible with green solder mask:
- Single-Sided Hole-Filling Compatibility: OSP's low-temperature treatment does not cause the green mask to peel off, and the organic film covers only the exposed copper foil without affecting the areas covered by the green mask; therefore, a single-sided via plugging design is acceptable.
- Important Notes: The OSP protective layer has a relatively short shelf life (typically 6 months). If a customer’s PCB needs to be stored for an extended period, it must be vacuum-sealed after single-sided via plating and include a desiccant to prevent the solder mask and OSP layer from aging together.
Suitable Scenarios: OSP is suitable for cost-sensitive PCB products with short production cycles, such as those used in consumer electronics (e.g., home appliances and toys). If the customer’s requirements for VIA via-hole solder mask design are simple (e.g., single-sided openings), OSP can serve as a cost-effective surface treatment option.
(4) Electroless Silver Plating (ENIAg): A “Balanced Solution” for Applications with Moderate Reliability Requirements”
The silver plating process forms a silver layer (0.1–0.3 μm thick) on the surface of a PCB through chemical deposition. It features good electrical conductivity and excellent solderability. The process temperature is approximately 70–85°C, and its compatibility with solder mask falls between that of gold plating and OSP:
- Feasibility of Single-Sided Hole Plugging: The low-temperature properties of silver plating make it suitable for single-sided VIA plugging designs; however, the risk of “silver migration” must be taken into account — — If a PCB is exposed to a high-humidity environment for an extended period (relative humidity > 60%), the exposed silver layer may undergo an electrochemical reaction with the copper foil at the edges of the solder mask, forming conductive silver filaments that can cause short circuits.
- Optimization Suggestions: If the customer chooses a silver plating + single-sided blind via design, a “solder mask bridge” (a solder mask isolation strip with a width of ≥0.1 mm) must be added along the edge of the solder mask window to reduce the contact area between the silver layer and the copper foil. We also recommend that the customer control environmental humidity during product use to prevent silver migration.
Suitable Scenarios: Immersion silver plating is suitable for PCB products with moderate reliability requirements, such as those used in industrial control and automotive electronics. If a customer requires single-sided via exposure and the operating environment has controlled humidity, immersion silver plating is a choice that balances performance and cost.
Surface Treatment and Green Oil Window Process Compatibility Chart
|
Surface Treatment Methods
|
Adapted for the "Green Oil Window" Process
|
Prohibited / Use with Caution Processes
|
Core Strengths
|
Applicable Scenarios
|
|
Hot Air Solder Leveling (HASL)
|
Double-sided plug holes, fully open windows
|
Single-sided plug holes
|
Low cost, high protection
|
Consumer electronics, low-end industrial equipment
|
|
Electrolytic Nickel-in-Gold (ENIG)
|
Single-sided plugged holes, with localized openings
|
无
|
High-temperature resistance, high reliability
|
Medical Devices, Communication Modules
|
|
OSP
|
Single-sided plug holes, fully open windows
|
Local Window Opening (High Precision Required)
|
Low cost, lead-free, and environmentally friendly
|
Home Appliances, Toys
|
|
Silver Plating (ENIAg)
|
Single-sided plugged holes, with localized openings
|
Single-sided plugging in high-humidity environments
|
Good electrical conductivity and excellent weldability
|
Industrial Control, Automotive Electronics
|
III. Design Review for Green Oil Windows: A Critical Step from “Customer Requirements” to “Technical Implementation”
Once the surface treatment method has been determined, the manufacturer must conduct a detailed review of the green-oil window design documents provided by the customer, focusing on identifying “potential process risks,” and communicate with the customer to develop optimization plans to avoid rework during later stages of production. The review should focus on the following key areas:
(1) VIA Hole Solder Paste Coverage: Avoid Designs Where “Solder Paste Covers the Hole Opening”
Customers often request that the green solder mask completely cover the VIA openings (i.e., that the edge of the green solder mask be flush with the opening) for “aesthetic” or “protective” reasons; however, this design can easily lead to two major problems during production:
- The Hidden Dangers of Sesizhu: Regardless of the surface treatment used, the holes in the green solder mask will result in a “gap” at the junction between the hole and the solder mask; if the subsequent soldering temperature is too high, solder is likely to seep into the gap, forming solder balls;
- Green-on-Green Peeling Risk: Stress concentration occurs at the interface between the substrate and the copper foil around the hole opening, and the solder mask covering the hole opening exacerbates this stress. During subsequent machining operations (such as cutting or drilling), the solder mask is prone to peeling away from the hole opening.
Optimization Suggestions: After consulting with the client, the design was changed from “green solder covering the hole opening” to “green solder flowing into the hole” — — This allows the green solder mask to flow naturally into the hole (to a depth of ≤1/3 of the hole depth), while leaving a 0.1–0.2 mm exposed area around the hole opening (i.e., a “tin ring”). This design ensures the protective function of the green solder mask while preventing the formation of gaps and reducing the risk of solder balls.
(2) Local windowing accuracy: Keep the “window deviation” within the specified range
When a customer requests a local cutout for a VIA hole, the dimensional accuracy of the cutout area must be verified to ensure compliance with PCB manufacturing standards (IPC-6012):
- Minimum Window Opening Size: The exposed area of a local opening must be ≥0.2 mm × 0.2 mm (i.e., 8 mil × 8 mil); if it is smaller than this size, the effective soldering area of the pad will be insufficient, which will affect soldering reliability;
- Deviation in Window Placement: The deviation between the center of the local opening and the center of the VIA hole must be ≤0.1 mm (4 mil). If the deviation is too large, it may cause the green solder mask to cover critical paths or expose too much copper foil;
- Width of Lüyou Bridge: If multiple VIA holes are adjacent and all use local openings, the width of the solder mask bridge between adjacent opening areas must be ≥0.1 mm (4 mil) to prevent the bridge from breaking due to excessive narrowness, which could cause a short circuit.
Review Tools: Use CAD design software (such as Altium Designer or AutoCAD) to perform layer analysis on the Gerber files provided by the customer, noting any deviations in the dimensions and positions of the cutouts. If these deviations exceed the standard range, prepare a “Design Optimization Report” that includes the standard requirements and a risk assessment, and consult with the customer to make adjustments.
(3) “Symmetry” of Single-Sided Window Openings: Avoiding “Uneven Stress on One Side”
For VIA single-sided window designs, the selection of the window surface and the symmetry of the green solder mask coverage must be reviewed:
- Compatibility with Window Openings: If the PCB is a multilayer board, when cutting a window on one side, ensure that the side with the window matches the side where soldering will take place—for example, if the customer is soldering on the front side of the PCB, the window should be cut on the front side to avoid cutting it on the back side, which would prevent the solder from making contact with the traces inside the holes during soldering;
- Green Cover Symmetry: Even with single-sided vias, the solder mask coverage must remain symmetrical to prevent uneven distribution of the solder mask within the vias, which could cause stress imbalance when the PCB is heated and result in warping.
Case Studies: A customer designed single-sided via windows (reverse-side windows) for a multilayer communication board, but subsequent soldering had to be performed on the front side, resulting in poor electrical continuity within the vias after soldering. After reviewing the design and identifying the issue, the manufacturer recommended that the customer change the configuration to “front-side windowing with partial solder mask coverage” and adjust the solder mask fill depth. This ultimately resolved the conductivity issue, reducing the defect rate from 25% to 3%.
IV. The “Best Solution” for the “Green Window” Issue: Process Optimization and Scenario Adaptation
Based on the type of surface treatment and the results of the green solder mask window design review, manufacturers can choose either the “double-sided via-filling process” or the “tin ring around the green solder mask window” as the core solution. The applicable scenarios, key operational points, and advantages of these two approaches are as follows:
(1) Double-Sided Plugging Process: The “Preferred Solution” for Applications Requiring High Reliability”
The double-sided via plugging process involves using screen printing or vacuum via plugging equipment to simultaneously fill the via holes on both the front and back sides of the PCB with solder mask, achieving full coverage of the via holes. This is followed by processes such as pre-curing, exposure, development, and final curing to form a complete solder mask protective layer. This process is suitable for all surface finishes and is particularly well-suited for high-reliability PCB products:
- Core Strengths:
-
- No risk of solder balls: Full-hole green solder mask filling prevents voids inside the holes, ensuring that no molten solder seeps in or metal particles remain, regardless of whether the process involves spray tinning, electroless gold plating, or OSP;
-
- High Protection: Double-sided plugging completely isolates the VIA holes from the outside environment, effectively protecting against moisture, dust, and corrosive gases, and extending the PCB's service life;
-
- Structural Stability: The green solder mask is evenly distributed within the holes, reducing uneven stress on the PCB when it is heated and minimizing the risk of warping.
- Key Points for Operation:
-
- Green ink selection: Use a “high-filling photosensitive green ink” (such as the Sun Ink PSER-4000 series) to ensure that the green ink completely fills the holes without any air bubbles;
-
- Curing parameters: Pre-curing temperature should be maintained at 70–80°C for 15–20 minutes; final curing temperature should be maintained at 150–160°C for 60–90 minutes to ensure the green solder mask is fully cured and to prevent peeling later on;
-
- Hole Diameter Compatibility: Double-sided plugging is suitable for VIA holes with a diameter of ≥0.2 mm. If the hole diameter is <0.2 mm, vacuum plugging equipment must be used to prevent the solder mask from failing to fill the hole.
- Applicable Scenarios: PCB products with extremely high reliability requirements, such as those used in medical devices, aerospace, and automotive electronics, or scenarios where customers require VIA holes to be fully covered with green solder mask and have no openings.
(2) Tin Ring Process for the Edges of Green-Coated Windows: A “Balanced Solution” That Strikes a Balance Between Cost and Performance”
The “tin ring” process for green mask windows involves leaving a 1–2 mil (0.025–0.05 mm) exposed copper foil area around the edges of the VIA hole’s green mask window to form a “tin ring,” which is then coated with a surface treatment (such as tin plating or electroless gold plating). This process is suitable for designs with localized or single-sided windows:
- Core Strengths:
-
- Preventing Solder Beads: The presence of the solder ring creates a “buffer zone” between the green solder mask and the hole opening; even if molten solder seeps in during solder spraying, it will be guided to the surface by the solder ring, preventing the formation of solder beads inside the hole;
-
- Improving Soldering Reliability: The tin ring increases the effective area of the pad, allowing the solder to adhere better during the soldering process and reducing the risk of cold solder joints;
-
- Cost-effective: No need to add additional via-filling equipment; simply adjust the size of the openings in the green film, making it suitable for small- to medium-volume production.
- Key Points for Operation:
-
- Solder Ring Dimension Control: The width of the solder ring must be strictly controlled between 1 and 2 mil. If the width is less than 1 mil, it will not provide adequate protection; if the width exceeds 2 mil, it will expose too much copper foil, increasing the risk of oxidation;
-
- Surface Treatment Compatibility: In the tin-plating process, the tin ring forms a uniform tin layer; in the electroless gold plating process, the tin ring forms a nickel-gold layer. Both ensure good solderability;
-
- Visual Inspection: After production, AOI (Automated Optical Inspection) equipment must be used to check whether the solder ring is intact and to verify that there are no residues of green solder mask or unevenly exposed copper foil.
- Applicable Scenarios: PCB products for applications with moderate reliability requirements, such as consumer electronics and industrial control, or scenarios where customers require localized or single-sided cutouts and are cost-sensitive.
(3) Handling Special Situations: Matching the Type of Photosensitive Ink to the Process
It is important to note that both of the above methods are based on “standard photosensitive green solder mask” (UV-curable). If the customer uses “thermosetting green solder mask,” the process parameters must be adjusted to prevent the solder mask from failing:
- Properties of Thermosetting Green Enamel: Thermosetting green solder mask does not require UV exposure and cures at high temperatures (120–140°C), but it has poor flow properties, weaker filling capability than standard photoresist green solder mask, and lower compatibility with surface treatments;
- Recommendations for Process Adjustments:
-
- If using thermosetting solder mask, the double-sided via-filling process is not recommended; instead, you may opt for the “single-sided via-filling + solder ring” combination to reduce the amount of solder mask used;
-
- Thermosetting green mask has poor compatibility with the tin-spraying process and is prone to peeling; it is recommended to use it in combination with immersion gold or OSP surface treatment;
-
- Extended curing time: The final curing time for thermosetting green solder mask must be extended to 120–150 minutes to ensure complete curing and improve adhesion.
V. Manufacturers“ ”Customer Communication Strategies“: From ”Passive Acceptance“ to ”Active Guidance”
In addition to technical solutions, manufacturers must also establish an efficient customer communication mechanism to guide customers in optimizing the design of green-paint windows early in the project, thereby reducing production risks later on. Specific strategies are as follows:
(1) Provide the “Green Window Design Specifications Manual”
Distribute the standardized “PCB Solder Mask Window Design Specifications Manual” to customers in advance, clearly outlining the following:
- Design requirements for green solder mask windows corresponding to different surface treatments (e.g., tin plating prohibits single-sided via filling);
- Standard range for VIA hole dimensions (e.g., local opening area ≥ 0.2 mm × 0.2 mm);
- Examples of Common Design Errors (with Images of Defective Products) and Optimization Solutions;
- The manufacturer's process capability parameters (such as minimum solder ring width and maximum via diameter).
Use the manual to guide customers in avoiding risks during the design phase and reducing the cost of later revisions.
(2) Issuing a “Design Feasibility Assessment Report”
Within 24 hours of receiving the client’s design documents, we will issue a “Green Oil Window Design Feasibility Assessment Report,” which includes the following:
- Analysis of the Compatibility Between Surface Treatment and Green Oil Window Design;
- Potential risk factors (e.g., Sesizhu, peeling of green paint) and risk levels (high / medium / low);
- Optimization Recommendations (with revised design drawings);
- Optimized cost and timeline estimates.
Reports should include data and visualizations to help clients clearly understand the need for optimization (e.g., “If no adjustments are made, the defect rate is projected to reach 151 TP3T, and the delivery cycle will be extended by 3 days”).
(3) Providing “Sample Testing Services”
For high-value or complex PCB orders, we offer a “sample testing service”:
- Based on the customer’s original design and the manufacturer’s optimized design, produce 2–5 samples;
- Perform surface treatment, welding tests, and high- and low-temperature cycling tests on the samples, and issue test reports;
- Show clients the differences in appearance and performance between the two design prototypes, and use data to demonstrate the advantages of the optimized solution.
Conduct sample testing to build customer confidence in the optimization plan and drive design adjustments.
VI. The “Quality Closed-Loop” in PCB Solder Mask Window Design”
To address customer issues regarding green-painted window designs, a closed-loop quality process must be established: “Surface Treatment Assessment → Design Review → Process Optimization → Customer Communication”:
- Preliminary Assessment: First, determine the type of surface treatment. The tin plating process must not involve single-sided via filling; electroless gold, OSP, and electroless silver can be used for single-sided or partial windowing;
- Thorough Review: Focus on identifying issues such as holes in the green oil cover, insufficient precision in localized cutouts, and asymmetry in single-sided cutouts, and prepare an optimization report;
- Process Selection:高可靠性需求选双面塞孔,中等需求选锡圈工艺,热固化绿油需调整参数;
- 主动沟通:通过规范手册、评估报告、样品测试,引导客户优化设计,平衡需求与可行性。
在电路板制造行业,绿油窗设计的细节处理直接决定产品质量与客户满意度。制造商需以技术为核心,以沟通为桥梁,将 “客户痛点” 转化为 “质量亮点”,在满足个性化需求的同时,建立高效、可靠的生产体系。未来,随着 PCB 向高密度、高可靠性发展(如 5G 基站、新能源汽车 PCB),绿油窗工艺将进一步升级,制造商需持续关注行业技术动态,优化解决方案,为客户提供更优质的产品与服务。