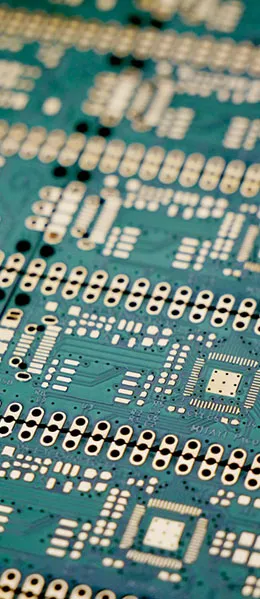
The traditional PCB industry has focused on miniaturizing conventional substrates and laminate materials, as well as increasing the number of layers. However, challenges such as heat dissipation, the removal of excess material from circuit boards, and the coefficient of thermal expansion (CTE) have led the industry to seek alternative materials better suited to addressing these issues. This has led to the adoption of ceramic materials.
Advantages of Ceramics
Ceramic materials, such as aluminum oxide, aluminum nitride, and beryllium oxide, outperform traditional laminates—such as polyimide, polystyrene, epoxy-glass fiber, and phenolic resin—in terms of thermal conductivity, corrosion resistance, and CTE. Ceramic materials also excel in component compatibility and high-density trace routing, making them particularly well-suited for applications such as High-Definition Multimedia Interface (HDMI) connections. These characteristics make ceramic materials an ideal choice for manufacturing multilayer boards.
Alumina Ceramic Substrate
Alumina ceramic substrates are widely used in multilayer ceramic substrates, electronic packaging, and high-density packaging substrates due to their high mechanical strength, excellent electrical insulation, and light-blocking properties. However, there are currently some issues in the domestic production of alumina ceramic substrates, such as excessively high sintering temperatures, which has led to China’s heavy reliance on imports for this critical component.
Alumina has several polymorphs, such as α-Al₂O₃, β-Al₂O₃, and γ-Al₂O₃. Among these, α-Al₂O₃ is the most stable and offers the advantages of high density and mechanical strength, making it widely used in industry. Alumina ceramics can be classified based on their purity; those with a purity exceeding 99% are referred to as corundum ceramics, while those with purities around 99%, 95%, and 90% are called 99 ceramics, 95 ceramics, and 90 ceramics, respectively; those with a purity exceeding 85% are generally referred to as high-alumina ceramics. These different types of alumina ceramics possess distinct properties in terms of density, flexural strength, linear expansion coefficient, thermal conductivity, and dielectric strength, enabling them to meet a wide range of application requirements.
Black Aluminum Oxide Ceramic Substrate
Black alumina ceramic substrates are widely used in semiconductor integrated circuits and electronic products. This is primarily because many electronic products are highly light-sensitive and require packaging materials with strong light-blocking properties to ensure the clarity of digital displays. Therefore, black alumina ceramic substrates are highly favored in electronic product packaging. When selecting black pigments, it is necessary to consider the properties of the ceramic raw materials, such as electrical insulation, thermal insulation, and other functional characteristics. During the ceramic coloring process, low-temperature environments may affect the volatility of the pigments; therefore, a certain holding time is required to ensure effective coloring.
Different Types of Ceramic PCBs
Ceramic PCBs include thick-film ceramic PCBs, low-temperature co-fired ceramic (LTCC) PCBs, and high-temperature co-fired ceramic (HTCC) PCBs, among others. Each type has its own unique applications and characteristics.
Thick-Film Ceramic PCBs
These circuit boards consist of gold and dielectric pastes printed onto a ceramic substrate and are fired at a temperature slightly below 1,000°C. Thick-film ceramic PCBs can use either gold or copper, but copper is used most frequently due to its lower cost. To prevent oxidation, the board is fired in a nitrogen atmosphere.
Low-Temperature Co-fired Ceramic (LTCC) PCB
LTCC uses co-firing, which involves simultaneously firing materials such as non-glass materials, glass composites, or glass crystals. The traces are typically made of gold to achieve high thermal conductivity, and the circuit board is fired at 900°C.
High-Temperature Co-fired Ceramic (HTCC) PCB
HTCC uses alumina and a binder, as well as plasticizers, solvents, and lubricants. The circuit traces can be made of metals such as tungsten and molybdenum, and the sintering temperature can range from 1,600°C to 1,700°C. This method is best suited for small circuit boards and carrier circuits.
Applications of Ceramic Multilayer PCBs
Ceramic multilayer PCBs perform exceptionally well in high-speed, high-power circuit applications. Compared to traditional PCB materials, these boards can reduce parasitic capacitance by up to 90%, offering great promise for future applications in the aerospace, medical device, industrial, and automotive sectors. iPcb® is a professional manufacturer of high-precision PCBs, capable of mass-producing 4- to 46-layer PCBs, circuit boards, high-frequency boards, high-speed boards,HDI Board, PCBs, high-frequency and high-speed boards, double-sided and multilayer PCBs, HDI PCBs, mixed-voltage PCBs, high-frequency PCBs, rigid-flex PCBs, etc.
Pros and Cons
The main advantage of ceramic multilayer PCBs lies in their thermal properties. The most important of these is thermal conductivity, which far exceeds that of traditional materials. In the table below, we compare FR4—the most commonly used substrate—with ceramic multilayer boards.
| Features | Ceramic Multilayer PCBs | FR4 |
|---|---|---|
| Thermal Conductivity (W/m·K) | 高 | 低 |
| Mechanical Strength | 高 | 低 |
| Insulation Properties | Excellent | Good |
| Parasitic Capacitance Reduction Rate | Significant | Limited |
As shown in the table above, ceramic multilayer PCBs offer significant advantages in terms of thermal conductivity, mechanical strength, and reduction in parasitic capacitance, making them highly popular in high-performance circuit applications.
As an emerging material for printed circuit boards, ceramic multilayer PCBs offer outstanding thermal and mechanical properties, opening up vast possibilities for the future development of electronic products. With continuous technological advancements, ceramic PCBs will play an increasingly important role in the aerospace, medical device, industrial, and automotive sectors. Therefore, for professionals and manufacturers in the PCB development field, understanding and mastering the applications and advantages of ceramic multilayer PCBs will become crucial.